Ayar Labs and GUC Validate CPO Thermal Co-Simulation
Thermal co-simulation brings optical engines, ASICs, bridges and package cooling into one model before a co-packaged design reaches hardware.
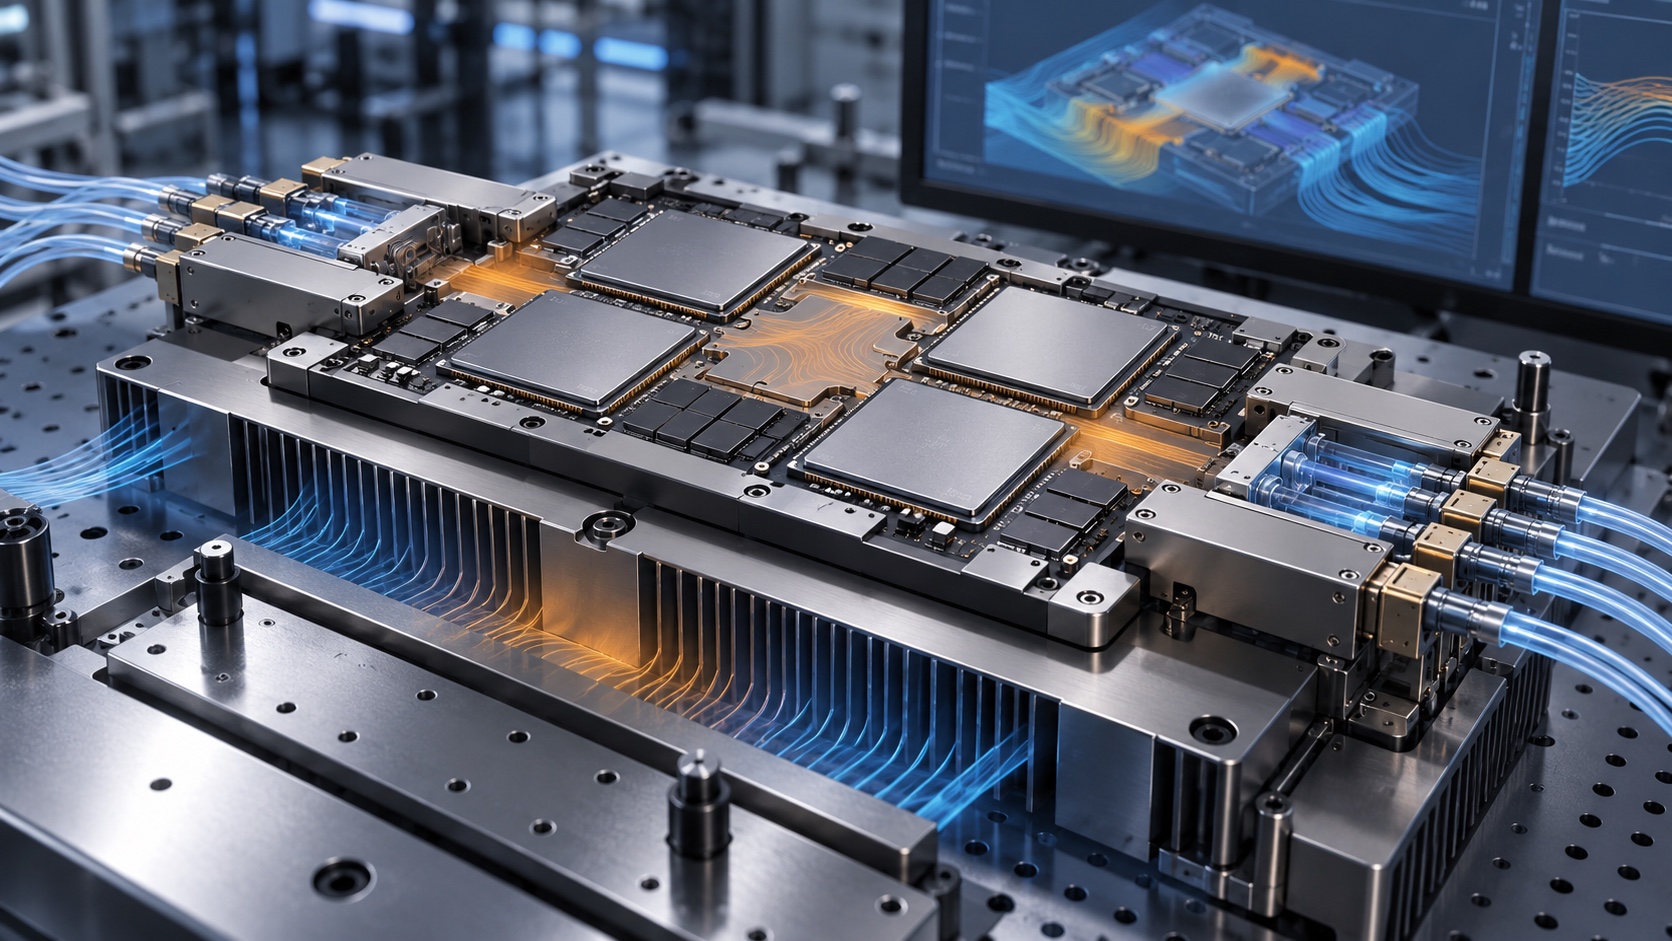
Thermal work moves earlier
Ayar Labs and Global Unichip reported thermal co-simulation of a multi-chip package integrating TeraPHY optical engines into an advanced ASIC and packaging workflow. The model considers optical I/O alongside compute silicon, local interconnect bridges and the package environment.
Optical engines sit close to high-power compute or switch dies, where local temperatures and gradients can affect lasers, modulators and reliability. Thermal planning therefore has to be part of architecture selection, not a late mechanical correction.
Simulation results need correlation with instrumented hardware across workloads, airflow conditions and manufacturing variation. Teams should verify junction temperatures, optical drift, coupling stability, aging margins and behavior during partial cooling failures.
The work illustrates how CPO pulls optical, ASIC, package and cooling suppliers into a shared design loop. Better co-simulation can reduce prototype cycles, but clear model ownership and measured correlation are essential before production sign-off.
Architecture and system boundaries
The significance of Ayar Labs and GUC Validate CPO Thermal Co-Simulation becomes clearer when it is evaluated as part of a complete link rather than as an isolated component. Thermal co-simulation brings optical engines, ASICs, bridges and package cooling into one model before a co-packaged design reaches hardware. A production design must account for the host SerDes, electrical channel, optical engine, connector, fiber plant, receiver and forward-error-correction behavior as one system. Improvements in one block can be lost through extra insertion loss, retiming power or thermal constraints elsewhere. Engineering teams should therefore document the intended reach, lane configuration, modulation, fiber type and environmental limits before comparing solutions. This boundary definition also prevents a laboratory demonstration, a reference design and a qualified product from being treated as equivalent stages of maturity.
Bandwidth density is valuable only when the surrounding platform can power and cool it reliably. Module or engine power should be measured at realistic traffic loads and temperatures, including the laser source, control electronics and any host-side retimers. Designers also need to consider airflow obstruction, heat-sink pressure, neighboring-port population and the effect of a failed fan or elevated inlet temperature. A lower headline wattage may not reduce facility power if it requires additional cooling or signal conditioning. Useful comparisons therefore include watts per transported bit, ports per rack unit, cooling margin and the number of fibers or connectors required for the same aggregate capacity.
A credible qualification plan combines electrical, optical, mechanical and software tests. It should cover transmitter quality, receiver sensitivity, stressed input tolerance, FEC margin, link startup, repeated hot insertion, temperature cycling and long-duration traffic. Multi-vendor testing is especially important when the host, module, cable assembly and management software come from different suppliers. Operators should record firmware versions and test limits so that later substitutions can be assessed against the same baseline. Compliance with a form factor or interface specification is necessary, but it does not guarantee that every host and optical implementation will deliver identical margin under real deployment conditions.
Operations and failure isolation
High-speed optics must be diagnosable after installation, not only during laboratory acceptance. Telemetry should expose temperature, supply voltage, transmit and receive power, lane alarms, FEC counters and relevant laser or DSP status through tools already used by the network team. Thresholds need to distinguish gradual degradation from immediate service risk. Documentation should explain how to isolate a dirty connector, damaged fiber, weak transmitter, marginal host channel or firmware mismatch without replacing multiple parts at once. Spare strategy and mean time to repair also matter: a dense architecture can save power and space yet increase outage duration if the failed optical element is difficult to access or replace.
Moving from a demonstration to repeatable volume production requires stable wafer processes, optical alignment, packaging, calibration and automated test. Buyers should ask whether quoted performance represents typical devices, selected samples or guaranteed production limits. Yield at the final assembly level can differ greatly from individual component yield because tolerances accumulate across lasers, photonic dies, fiber attach and electronics. Capacity claims should be reviewed together with qualified manufacturing locations, lead times, second-source options and change-control procedures. Traceability from finished module to critical components helps contain field issues and makes it easier to evaluate whether a design revision requires renewed system qualification.
Purchase price alone is an incomplete measure for a new optical architecture. A useful total-cost model includes switch ports, optics, fiber and patching, power, cooling, spares, installation time, test equipment and expected replacement labor. It should also reflect utilization: a higher-capacity link can be economical when traffic can fill it, but may strand capital when deployed too early. Contracts should separate sample specifications from production guarantees and define acceptance criteria, warranty handling and notification of material or firmware changes. Where the ecosystem is still developing, staged orders and interoperability gates can reduce risk while preserving access to supply.
Official source
Official source: https://ayarlabs.com/blog/ayar-labs-and-guc-complete-successful-thermal-co-simulation-testing-of-co-packaged-optics
Goilips summarizes the official announcement and adds industry analysis. Verify availability, specifications and qualification status before procurement.